





| Quantity: | |
|---|---|


S355J2
Qilu
Product Description
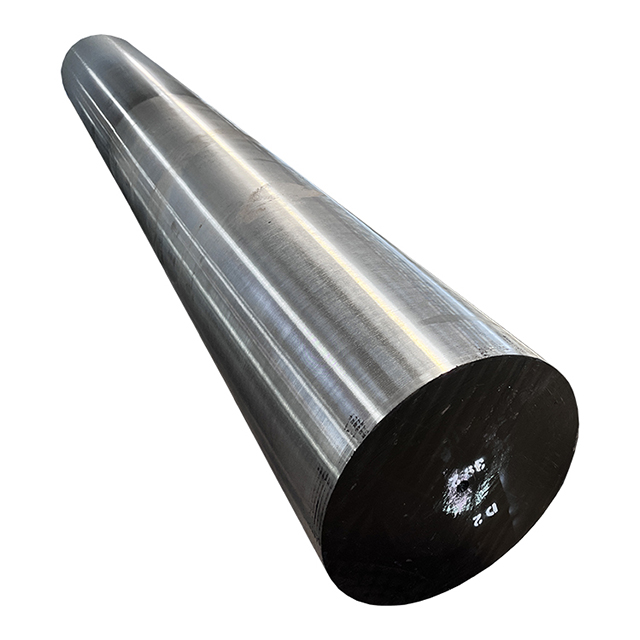
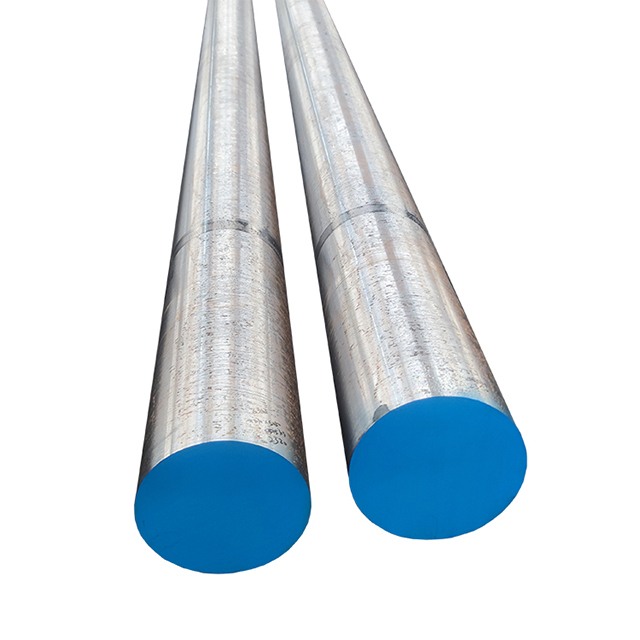
Q355D round bar from 20 mm to 500 mm, supplied hot rolled, forged or normalized, with 34 J Charpy results at −20 °C and EN 10204 3.1 documentation. This is the cold-region member of the Chinese 355 MPa structural class — the grade specified when a structure has to keep its toughness through a winter at −20 °C rather than only at room temperature.
Equivalent to: EN 10025-2 S355J2 (1.0577) · DIN 17100 St52-3N (superseded) · GB/T 1591-2018 Q355D · ASTM A572 Gr 50 class for strength only (no impact requirement in the ASTM base specification)
Q355 replaced Q345 in the 2018 revision of GB/T 1591. Drawings and old stock lists still say Q345D; the current designation is Q355D, and the guaranteed yield moved up 10 MPa in the change.

S355J2 round bar in stock
Product form: hot rolled round bar, hot forged round bar; peeled or turned and polished on request
Diameter range: 20 mm – 500 mm; lengths 3–6 m, cut to size on request
Delivery condition: as-rolled (+AR), thermomechanically rolled (TMCP) or normalized (+N)
Production route: BOF or EAF melting, ladle refining, VD/VOD where specified, continuous casting or ingot, rolling or forging
Standards: GB/T 1591-2018 (Q355D), EN 10025-2 (S355J2); dimensional tolerances by agreement
Certificates: EN 10204 3.1 with ladle analysis, tensile and Charpy results; 3.2 by arrangement
Testing: tensile per heat; Charpy V-notch 34 J at −20 °C for grade D; UT and grain size on request
Lead time: stock sizes ex-warehouse; rolled and forged diameters typically 20–35 days
Q355D is a microalloyed structural steel, not a through-hardening grade. Carbon sits at or below 0.20 % so the weld heat-affected zone does not harden into something brittle, and the strength comes from manganese plus small additions of niobium, vanadium or titanium working through grain refinement and precipitation. That is the whole design idea: reach 355 MPa without paying for it in weldability.
The grade letter D is bought with cleaner steel, not stronger steel. Carbon, phosphorus and sulfur all tighten as the letter moves from B to C to D to E, and grade D also expects fully killed, fine-grain practice with acid-soluble aluminium at 0.015 % minimum where fine grain is specified. A heat made to Q355B limits and stamped Q355D is not a paperwork slip — the certificate would have to show the tighter figures and the heat may not be there.
| Element, % (ladle analysis) | Q355B | Q355C | Q355D | Q355E |
|---|---|---|---|---|
| C, max | 0.24 | 0.20 | 0.20 | 0.18 |
| Si, max | 0.55 | 0.55 | 0.50 | 0.50 |
| Mn, max | 1.60 | 1.60 | 1.60 | 1.60 |
| P, max | 0.035 | 0.035 | 0.030 | 0.025 |
| S, max | 0.035 | 0.035 | 0.030 | 0.020 |
| N, max | 0.012 | 0.012 | 0.012 | 0.012 |
| Nb + V + Ti, max | 0.22 | 0.22 | 0.22 | 0.22 |
| Al (acid soluble), min | 0.015 | 0.015 | 0.015 | 0.015 |
Values are the GB/T 1591-2018 ladle-analysis limits for the as-rolled and normalized routes, quoted for thickness up to 16 mm. The microalloy total is a ceiling, not a requirement: two conforming Q355D heats can reach the same strength by quite different routes, one leaning on niobium with TMCP, the other on vanadium with a normalizing pass. That difference matters when a fabricator wants to re-normalize a bar that was already normalized — the second thermal cycle can coarsen what the first one refined.
The 355 MPa headline applies to sections up to 16 mm. Above that the requirement steps down as the section slows the cooling rate, and a buyer ordering 200 mm bar who quotes the small-section figure is quoting something no mill can certify. Read the row that matches the diameter on the order, not the number in the grade name.
| Thickness / diameter, mm | Yield ReH, min | Tensile Rm | Elongation A, min |
|---|---|---|---|
| ≤ 16 | 355 MPa | 470 – 630 MPa | 22 % |
| > 16 – 40 | 345 MPa | 470 – 630 MPa | 22 % |
| > 40 – 63 | 335 MPa | 470 – 630 MPa | 21 % |
| > 63 – 80 | 325 MPa | 470 – 630 MPa | 20 % |
| > 80 – 100 | 315 MPa | 470 – 630 MPa | 20 % |
| > 100 – 150 | 295 MPa | 470 – 630 MPa | 19 % |
| > 150 – 200 | 285 MPa | 450 – 600 MPa | 18 % |
| > 200 – 250 | 275 MPa | 450 – 600 MPa | 18 % |
| > 250 – 400 | 265 MPa | 450 – 600 MPa | 18 % |
Impact is where grade D earns its price. Q355D certifies Charpy V-notch energy of 34 J at −20 °C on longitudinal specimens, against 34 J at 0 °C for grade C and 34 J at −40 °C for grade E. Note the asymmetry with Europe before substituting one for the other: EN 10025-2 asks for 27 J at −20 °C in S355J2, so the Chinese grade commits to more energy at the same temperature, while the European thickness ladder above 63 mm diverges from the GB one. Where the design temperature drops to −40 °C, the grade to specify is Q355E; where the project also demands normalized delivery and a low-carbon weldable chemistry, the European equivalent is S355NL to EN 10025-3 rather than a GB grade, because GB/T 1591 does not define an NL class. The wider comparison of these ladders is set out in our article on S355 vs Q355 vs A572 Gr 50.
| System | Grade | Material number / note |
|---|---|---|
| GB/T 1591-2018 | Q355D | Chinese structural HSLA, 34 J at −20 °C |
| EN 10025-2 | S355J2 | 1.0577, 27 J at −20 °C |
| EN 10025-2 (normalized) | S355J2+N | 1.0577+N, normalized delivery |
| DIN 17100 (withdrawn) | St52-3N | Superseded by EN 10025-2; still seen on old drawings |
| ASTM | A572 Gr 50 | 345 MPa yield, no impact test in the base specification |
| ASTM (structural, older) | A36 | 250 MPa class — a different strength family, not a substitute |
| JIS G3106 | SM490B / SM490C | Welded-structure grades; check impact class separately |
Equivalent is a direction, not a swap. Moving from Q355D to S355J2 is usually acceptable to a European designer because the GB grade carries the stricter energy figure; moving the other way can fail a Chinese design code that expects 34 J. Moving from either to A572 Gr 50 changes the testing basis entirely, because the ASTM base specification does not require Charpy data at all. If the end user's inspection department is going to compare certificates, the grade on the certificate should be the grade on the drawing.
Bridge girders, cross beams and bearing components in cold-climate regions
Crane runways, gantry legs and lifting equipment subject to dynamic load
Transmission and communication towers, including galvanized lattice sections
Offshore and port structures: module frames, walkways, fender systems, mooring hardware
Mining and earthmoving equipment: axle housings, boom pins, chassis brackets
Heavy vehicle frames and suspension components where a weldable 355 MPa steel is required
General machined structural parts that are welded rather than heat treated
Q355D is welded far more often than it is machined, and the number that decides whether a weld procedure qualifies is carbon equivalent rather than yield strength. GB/T 1591-2018 caps CEV according to thickness, and the cap loosens as the section grows because thicker sections need more alloy to reach the same strength.
| Thickness, mm | CEV, max (Q355D) |
|---|---|
| ≤ 30 | 0.45 |
| > 30 – 63 | 0.47 |
| > 63 – 150 | 0.47 |
| > 150 – 250 | 0.49 |
Practical consequences for fabrication are the usual ones for a 0.45 CEV steel: preheat is not normally needed below about 20 mm in mild workshop conditions, it becomes advisable in the 20–40 mm range and around 100 °C for heavy sections, and it should be qualified by procedure rather than assumed. Hydrogen-controlled consumables matter more than most fabricators expect on thick bar, because the same section that needs preheat also restrains the weld. Where the finished part will be galvanized, note that silicon above roughly 0.30 % can produce a dark, uneven coating; if the appearance matters, specify the silicon ceiling at the order stage instead of discovering it at the pickling tank.
Delivery condition deserves the same explicit treatment. Hot rolled (+AR) is the normal supply and the cheapest; TMCP gets higher strength and better toughness out of a leaner chemistry; normalized (+N) gives a uniform ferrite-pearlite structure and is what most drawings mean by St52-3N. A normalized bar and an as-rolled bar of the same analysis do not machine identically and do not weld identically, so the condition belongs in the order description, not only in the grade designation.
Cutting, peeling, turning and centreless grinding to h9 / h11 tolerance on request
Sawing to fixed length with squareness checked before packing
In-house normalizing and stress relieving with recorded furnace charts
Spectrochemical analysis of every heat, with retained samples
Tensile and Charpy testing per heat, third-party witness arranged at order stage
Ultrasonic inspection against an agreed acceptance level for heavy sections
Export packing: seaworthy wooden cases, bundles strapped and edge-protected, mill certificates in the case
Documentation: EN 10204 3.1 as standard, 3.2 and customer-specific formats on request
A1: Close enough to be quoted against each other, not identical. Both guarantee 355 MPa yield in thin sections and both test at −20 °C, but GB/T 1591-2018 asks for 34 J where EN 10025-2 asks for 27 J, and the two standards use different thickness ladders above 63 mm. For a European project the S355J2 certificate is usually the easier document to place; for a Chinese design code the Q355D certificate is the one the reviewer expects.
A2: Yes, as Q355D. Q345 was withdrawn in the 2018 revision of GB/T 1591 and replaced by Q355, with the guaranteed yield raised by 10 MPa. Certificates issued against the withdrawn edition are still seen in the market; we issue to GB/T 1591-2018 and note the Q345 equivalence on the certificate when a customer's drawing still carries the old designation.
A3: Because the bar is over 16 mm. The 355 MPa figure applies up to 16 mm; 16–40 mm requires 345 MPa, 40–63 mm requires 335 MPa, and the ladder keeps stepping down to 265 MPa at 250–400 mm. On a 50 mm bar, 345 MPa is a conforming result, not a downgrade. If the design needs 355 MPa at a larger section, the grade has to move up rather than the tolerance be argued.
A4: Yes. Normalized Q355D is the direct replacement for the old DIN 17100 St52-3N designation, and we supply it with furnace charts and mechanical results from the normalized condition rather than from the as-rolled bar. For the fully normalized European route, the equivalent page is S355J2 / St52-3N round bar; the as-rolled 355 MPa grade is on the S355JR / Q355B page, and the −40 °C variant on the Q355E / S355K2 page.
Send the diameter, length, quantity, delivery condition and the certificate format your inspector expects, and we will quote against GB/T 1591-2018 Q355D or EN 10025-2 S355J2 — whichever ends up on the certificate. Mill test certificates, third-party inspection and cutting to length are quoted with the material rather than added afterwards.


