


| Quantity: | |
|---|---|


8620
Qilu
Product Description
Hot forged 8620 round bar supplied annealed for carburizing, 20 mm to 400 mm diameter, with rough machining and ultrasonic testing done in-house.
Equivalent to: AISI / SAE 8620 · DIN 21NiCrMo2 (1.6523) · JIS SNCM220 · GB 20CrNiMo
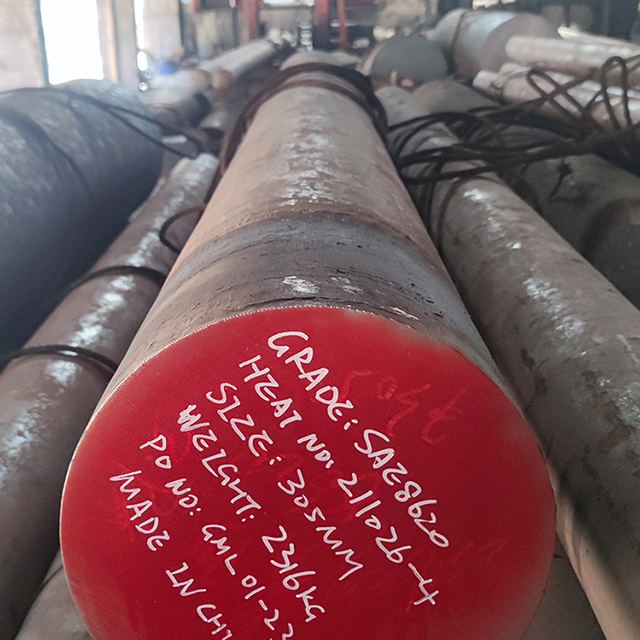
AISI 8620 Forged Round Bar in Stock
Supply form — Round bar, forgings, blanks
Process — Hot forged / hot rolled
Condition — Annealed for carburizing (≤ 229 HB)
Diameter range — 20–400 mm
Standard — ASTM A29 / SAE J404
Certificate — EN 10204 3.1 standard, 3.2 on request
Lead time — 20–35 days for forged sizes
8620 is the workhorse case-hardening steel of the AISI 86xx Ni-Cr-Mo family. The 0.40–0.70 % nickel lifts core toughness, the 0.40–0.60 % chromium and 0.15–0.25 % molybdenum give a hard, wear-resistant case after carburizing. It is the standard grade for carburized gears and bearings where you need a hard surface and a tough core.
| Grade | C | Mn | Si | P | S | Ni | Cr | Mo |
| 8620 | 0.18-0.23 | 0.70-0.90 | 0.15-0.30 | 0.035Max | 0.040Max | 0.40-0.70 | 0.40-0.60 | 0.15-0.25 |
8620 is supplied annealed and carburized by the buyer. Properties below show the annealed bar and typical case-hardened performance.
| Property | Annealed | Case-hardened |
| Tensile strength, Rm (MPa) | ≤ 640 | ≥ 980 (core) |
| Yield strength, Re (MPa) | ≤ 380 | ≥ 780 (core) |
| Elongation, A5 (%) | ≥ 17 | ≥ 8 (core) |
| Impact, KV (J) | ≥ 40 | ≥ 30 (core) |
| Surface hardness | ≤ 229 HB | 58–63 HRC (case) |
| Standard | Grade |
| ASTM / SAE (USA) | 8620 / 8620H |
| DIN (Germany) | 21NiCrMo2 / 1.6523 |
| JIS (Japan) | SNCM220 |
| GB (China) | 20CrNiMo |
| BS (UK) | 805A20 |
| EN (Europe) | 21NiCrMo2 / 1.6523 |
Gears — carburized transmission gears, pinions, ring gears
Bearings — roller bearings and races
Automotive — differential gears, camshafts, bushings
Heavy equipment — splined shafts, clutch hubs
8620 is carburized at 900–925 °C, then quenched (directly or after a sub-critical anneal) and tempered at 150–200 °C. The result is a 58–63 HRC case over a tough, ductile core. We supply the bar annealed and ready for your carburizing; for repeat production we can also deliver pre-rough-machined blanks cut to the gear blank size you need.
Most suppliers in this business are traders who subcontract everything. We run our own processes, which means shorter cycles and one point of accountability when something needs fixing.
Heat treatment shop — quenching and tempering to your target hardness, with furnace charts recorded per batch
Machining shop — rough turning, peeling and cutting to length, so your bar arrives ready for finish machining
Testing — ultrasonic per ASTM A388 / EN 10228-3, hardness mapping across the section, tensile and impact testing
Certification — EN 10204 3.1 as standard, 3.2 available with third-party witness (ABS, BV, CCS, GL)
Export packing — bundled, end-capped and rust-protected for sea freight
A1: 4320 has higher nickel (1.65–2.00 %) and is used for larger gears needing tougher cores; 8620 is the economical choice for most passenger-vehicle and light-truck gearing.
A2: Yes — 8620H with H-band chemistry is available on request, with the hardenability Jominy curve reported on the certificate. This is the common spec for repeat gear production where case depth must be controlled.
A3: Yes. We rough-turn and cut to length so you receive blanks ready for carburizing — this saves machining time and material loss in your own shop.
Send us your diameter, length, quantity, required hardness and destination port. You will get a quotation with the full technical proposal within 24 hours.


